GE
RFQ Ready
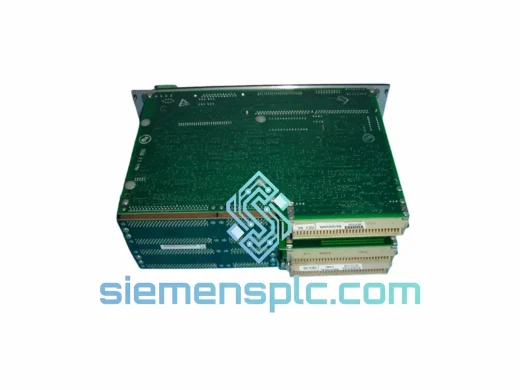
GE IS200VTCCH1CBD Thermocouple Processor Board – Mark VI IS200 Series
Mark VI
Origin US
Thermocouple Processor Board
Request verified availability, condition, replacement risk review, packing options and courier lead time for IS200WETBH1BAA.
Click Request Quote and the part number is inserted into the inquiry form automatically.
Core fields for model confirmation and RFQ routing. Detailed product narrative remains below.
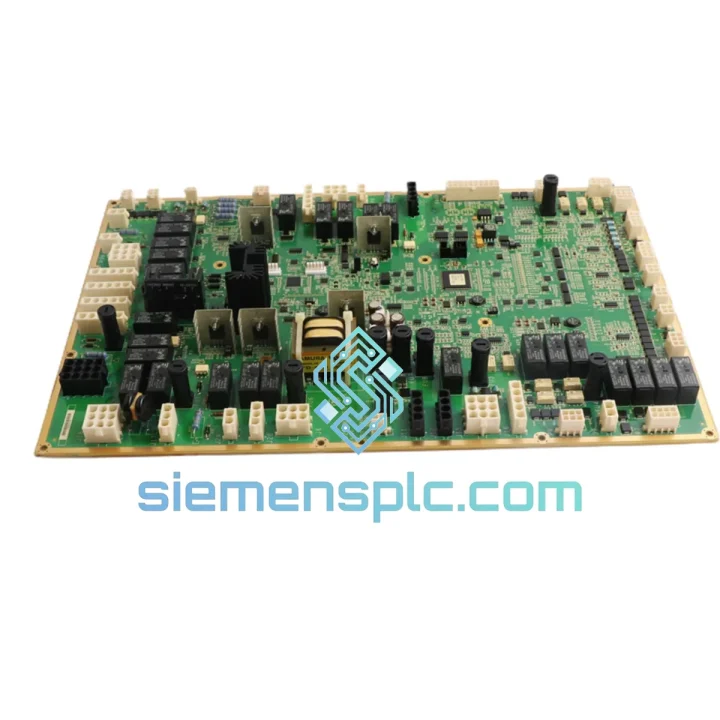
Your elevator is down. The Mark VI controller is throwing faults. Your maintenance team has already pulled the IS200WETBH1BAA and confirmed it’s the culprit. You don’t need a lecture on the product — you need a replacement on a plane tonight. That’s exactly what we do.
We stock the GE IS200WETBH1BAA at our Xiamen warehouse. Verified, bench-tested, and ready to dispatch via DHL or FedEx within hours of order confirmation. Whether you’re running a turbine hall service lift, a high-rise traction elevator, or a freight hoist in a petrochemical facility, this board goes back in the rack and your system comes back online. No weeks-long OEM lead time. No excuses.
URGENT REQUIREMENT? Contact: [email protected] | WhatsApp: +86 18359268345
| Part Number | IS200WETBH1BAA |
| Manufacturer | GE (General Electric) |
| Platform / Series | Mark VI Turbine & Excitation Control |
| Function | Elevator Control Board — motion sequencing, safety relay logic, floor-level position feedback |
| Form Factor | PCB module, Mark VI backplane-mount |
| Supply Voltage | 24 VDC nominal |
| Communication Bus | Mark VI internal backplane; GE Toolbox compatible |
| Operating Temperature | 0 °C to +60 °C |
| Humidity | 5% to 95% RH, non-condensing |
| Weight (as shipped) | 1,560 g |
| Condition | New OEM / Tested Surplus |
| Stock Status | ✔ READY TO SHIP — Xiamen Warehouse |
| Dispatch | Same-day if order confirmed before 14:00 CST |
| Warranty | 12 months against defects |
Fifteen years of field calls on Mark VI systems teach you the same lesson every time: the IS200WETBH1BAA fails in predictable ways. Here’s what to check before you pull the board — and what to do when you confirm it’s dead.
Common Fault Signatures:
Replacement Procedure — Field Checklist:
Firmware Note: The IS200WETBH1BAA does not carry user-flashable firmware in the traditional sense — its logic is tied to the Mark VI system software version. Confirm your Mark VI software revision with GE Toolbox before ordering if your system is running a non-standard software build. We can verify compatibility before dispatch.
The IS200WETBH1BAA was not designed for a climate-controlled server room. It was built for the environments where elevators actually operate — turbine halls with 55 °C ambient temperatures, offshore platforms with salt-laden air, mining headframes with constant vibration from winding gear, and petrochemical facilities where the air carries corrosive particulates.
GE’s Mark VI platform was engineered to MIL-spec-influenced design standards. The IS200WETBH1BAA PCB uses conformal coating on production variants to resist moisture ingress and condensation cycling. The backplane connector system is rated for thousands of insertion cycles without contact degradation. Onboard components are selected for extended temperature range operation, not consumer-grade tolerances.
In practice, these boards run for 10 to 15 years in service before failure — and when they do fail, it’s almost always a single component (a relay, a capacitor, a connector) rather than a catastrophic board failure. That’s why a tested surplus unit from our stock is a legitimate, cost-effective replacement: the board itself has decades of service life remaining.
Every unit we ship has been subjected to a full bench test protocol: power-on verification, backplane communication check, relay output actuation test, and encoder feedback path continuity. We don’t ship boards that haven’t passed. If it leaves our warehouse, it works.
Our dispatch hub is in Xiamen, China — one of the most connected export ports in Asia, with direct DHL and FedEx service to every major industrial hub on the planet. Here’s how the process works from the moment you confirm your order:
We have shipped GE Mark VI boards to power plants in Germany, refineries in Saudi Arabia, mining operations in Australia, and data centers in Singapore. The logistics process is not new to us. Your part will arrive intact, on time, and with full documentation for your maintenance records.
Email: [email protected]
WhatsApp: +86 18359268345
Web: siemensplc.com
© 2026. All rights reserved.
We check the full part number, brand, series and visible nameplate information before quotation.
Sales confirms stock path, condition option, quantity and realistic lead time for export dispatch.
DHL, FedEx, UPS or buyer courier arrangements can be reviewed with packing requirements.
Similar brand or category products for fast comparison and multi-item RFQ lists.